7 Belt Counterweight Scale Buying Tips
Choosing a Belt Counterweight Scale is not simply a matter of comparing prices. It is a practical decision about accuracy, belt movement, material flow, and daily maintenance. A reliable scale should remain stable when bulk materials create vibration, dust, or uneven loading. Small errors can grow quickly when a conveyor runs for many hours.
This guide presents seven buying tips based on common weighing challenges in mining, aggregates, recycling, and manufacturing environments. It considers frame strength, load-cell quality, speed measurement, calibration access, signal processing, and supplier support. Look closely at the installation area. A scale mounted near a transfer point may experience impact, spillage, and belt misalignment. Those conditions can change performance.
Details matter.
Experienced operators also know that specifications do not tell the whole story. A high-resolution indicator cannot correct poor belt tracking. Likewise, a strong frame may not compensate for careless installation. Every site has different temperatures, materials, belt tensions, and maintenance habits. Some recommendations may need adjustment after testing actual operating conditions. That is where careful verification becomes valuable.
The right Belt Counterweight Scale should provide dependable readings without creating unnecessary downtime. Ask for documented accuracy, calibration procedures, maintenance requirements, and application references. Confirm how the supplier handles troubleshooting after installation. A confident salesperson is useful, but clear technical evidence is better. These seven tips will help buyers compare equipment realistically and avoid decisions based only on attractive features or a low initial quotation.
Define the Weighing Requirements for Your Belt Conveyor
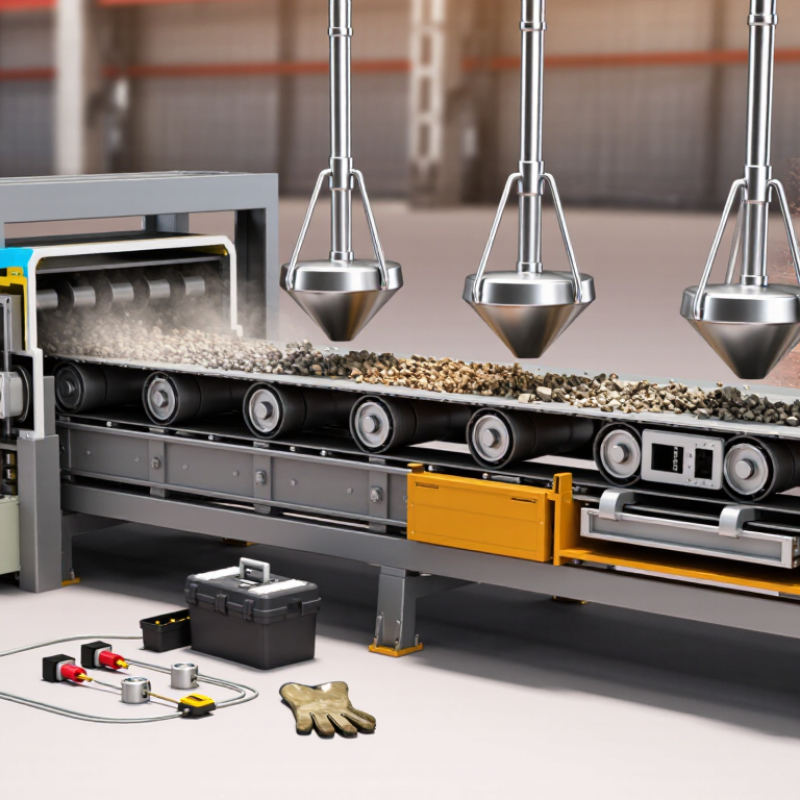
Before choosing a belt counterweight scale, define what must be weighed. Record the material type, moisture range, bulk density, particle size, and flow pattern. These details affect loading stability and measurement error. The U.S. Geological Survey estimated 1.5 billion metric tons of crushed stone and 960 million metric tons of sand and gravel were produced in 2023. Such materials can shift density during operation. A single design value may be misleading.
Measure the conveyor’s minimum, normal, and peak capacity. Include belt width, belt speed, incline, idler spacing, and expected daily operating hours. The CEMA Belt Conveyors for Bulk Materials handbook identifies belt speed, material density, surcharge angle, and loading conditions as key capacity factors. Specify required accuracy separately from repeatability. They are not identical. Also define whether the scale supports process control, inventory management, or commercial transactions.
Site conditions matter. Check dust, vibration, rain, temperature changes, belt tracking, and available straight belt length. The scale should match the conveyor structure, not only the target tonnage. For regulated weighing, NIST Handbook 44 provides reference tolerances and test procedures for weighing devices in the United States. Local rules may differ. I would also request calibration records, test-weight access, and a commissioning plan. A neat specification can still fail when material builds beneath the belt. Leave room for inspection, cleaning, and honest rechecking.
Match Counterweight Scale Capacity to Material Flow
7 Belt Counterweight Scale Buying Tips
Match the scale’s rated capacity to actual material flow, not the conveyor’s maximum nameplate speed. Measure average flow, peak surges, moisture changes, and start-up loading. A scale sized too low may overload during a wet-ore surge. An oversized scale can reduce resolution during light loading. That trade-off is easy to miss.
The U.S. Geological Survey’s Mineral Commodity Summaries 2024 reported about 22 million metric tons of mined copper production in 2023. Such high-volume operations need stable measurement across long production shifts. Use that scale when sizing equipment. Convert annual or daily tonnage into tonnes per hour, then add a realistic peak allowance. Do not simply add 50 percent. Review the loading profile first. A 600 t/h conveyor may regularly carry 420 t/h, yet briefly exceed 700 t/h during feeder release.
Check the counterweight, weigh-frame stiffness, belt tension, and speed range together. OIML R 50-1:2016 defines accuracy classes for continuous totalizing weighing instruments, so verify the required class before purchase. CEMA belt-conveyor guidance also emphasizes consistent belt conditions and proper alignment. Ask for calibration procedures using certified test weights or material tests. Confirm the instrument handles your smallest sustained flow, not only the largest one. Field errors often begin with poor loading placement. I have seen commissioning teams blame electronics when the belt was tracking against the structure. That happens. Leave access for inspection, clean the weigh area, and record flow, speed, and moisture during acceptance testing.
Belt Counterweight Scale Buying Tips: Match Scale Capacity to Material Flow
Select a counterweight belt scale with a rated capacity above the expected peak flow, while keeping normal operation within the middle portion of the measuring range. The example uses a 20% design margin above peak flow to accommodate surges, material-density variation, and future throughput increases. Actual selection should also consider belt width, belt speed, idler spacing, loading profile, moisture, and required accuracy.
Check Belt, Conveyor, and Installation Compatibility
7 Belt Counterweight Scale Buying Tips
Check Belt, Conveyor, and Installation Compatibility
When purchasing a belt counterweight scale, compatibility deserves more attention than headline capacity. The belt must suit the scale’s load cells, idler geometry, width, speed, and material profile. A narrow belt carrying sticky material can create unstable loading and uneven measurement. CEMA’s Belt Conveyors for Bulk Materials, Seventh Edition, links weighing performance with belt tension, alignment, idler condition, and loading consistency. Ask for the required accuracy at normal flow, not only maximum capacity. NIST Handbook 44, Section 2.21, specifies controlled tests for belt-conveyor scales and emphasizes repeatability under operating conditions. That matters.
Conveyor compatibility is equally practical. Check belt speed, incline, pulley spacing, skirtboards, dust, vibration, and available straight-run length before ordering. ISO 5048 calculations use belt mass, material flow, lift, speed, and conveyor resistance. Those inputs should match the site survey. Installation can fail quietly. A misplaced idler or loose structure may pass a visual check but distort readings. Follow alignment tolerances, then verify zero and span with certified test weights or a material test. Apply OSHA guarding and lockout requirements during installation and service. Do not guess. One imperfect assumption remains common: buyers often size the scale from peak throughput. Actual operations may run below design load, where belt tracking and material distribution become more influential. Review at least one week of operating data, if available, and document every change.
Compare Accuracy, Calibration, and Maintenance Features
When buying a belt counterweight scale, compare accuracy under real material conditions, not only the brochure’s best-case number. OIML R 50-1 identifies accuracy classes of 0.25, 0.5, 1, and 2 percent for continuous totalizing weighers. A tighter class may suit high-value materials, but it can demand better installation and belt control. Ask for test results at low, normal, and maximum flow rates.
Calibration matters just as much.
NIST Handbook 44 emphasizes repeatable testing, suitable test loads, and tolerances for weighing equipment used in trade. Choose a scale with an accessible calibration routine, stored test records, and clear zero-setting controls. Automatic zero tracking helps, but it should not hide persistent drift. Watch the empty belt.
Maintenance features often decide long-term accuracy. Look for sealed load cells, protected speed sensors, and simple access to the counterweight assembly. A practical system should show belt slip, zero deviation, and signal instability before readings become unreliable. OIML R 50-1 also stresses installation conditions and periodic verification, so calibration cannot repair poor alignment or material buildup. In my experience, cleaning plans are often underestimated. A small buildup near the weigh area can change tension and distort results. Choose inspection points that one technician can reach safely, without dismantling half the conveyor.
Evaluate Supplier Support, Safety, and Total Ownership Cost
7 Belt Counterweight Scale Buying Tips
A belt counterweight scale is only as reliable as its support network. Ask how quickly technicians respond when readings drift or the belt starts tracking unevenly. Request commissioning records, calibration procedures, wiring diagrams, and operator training. Practical support matters. Confirm spare load cells, rollers, cables, and counterweight parts are available locally. Ask whether remote diagnostics can identify faults before production stops.
Safety deserves direct inspection, not a checkbox. Check guarding around moving belts and counterweight assemblies. Verify emergency stops, overload protection, isolation points, and safe access for cleaning. The supplier should provide a documented risk assessment and clear maintenance instructions. Confirm the scale suits your belt speed, material flow, and surrounding conditions. An experienced supplier will explain limitations instead of promising perfect accuracy.
Total ownership cost extends far beyond the purchase price. Include installation, structural changes, calibration visits, software updates, energy use, and planned downtime. Compare expected maintenance hours over five years. Ask for accuracy data from similar applications, not only laboratory figures. I once saw a low-cost scale require frequent manual checks, which erased its initial savings. That experience still shapes my evaluations. A simple spreadsheet helps, although estimates can be imperfect. Use conservative downtime costs and record every assumption. Supplier references should include measurable results, service history, and unresolved problems. Reliability is demonstrated over time, not claimed in a quotation.