How to Choose the Right Roller Checkweigher?
Choosing a Roller Checkweigher is not just a matter of matching belt width to package size. The right system must handle your product’s weight range, line speed, packaging format, and washdown conditions. A damp carton and a rigid tray behave differently on rollers. So do products that arrive unevenly spaced. Small details matter.
PMMI’s 2024 State of the Industry report discusses ongoing packaging-industry pressures around labor, productivity, and operational performance. These pressures make dependable in-line inspection increasingly important, but a faster machine is not automatically a better fit. OIML R 51-1:2019 provides technical requirements for automatic catchweighing instruments, offering a useful reference when reviewing weighing performance and instrument design. These sources help frame the decision; your actual product trials should guide it.
A practical selection starts with real production conditions. Record typical and maximum line speeds, package dimensions, weight variation, and available floor space. Then check roller pitch, transfer gaps, reject timing, control-system compatibility, and access for cleaning. Ask suppliers how they verify accuracy under your specific operating conditions, and request results using representative products. A brochure cannot reproduce your line. That is worth remembering.
The choice may still involve trade-offs. A compact unit can save space but limit future flexibility. This guide explains how to compare key specifications, test a Roller Checkweigher, and select equipment that supports reliable, consistent inspection without overlooking everyday operating realities.
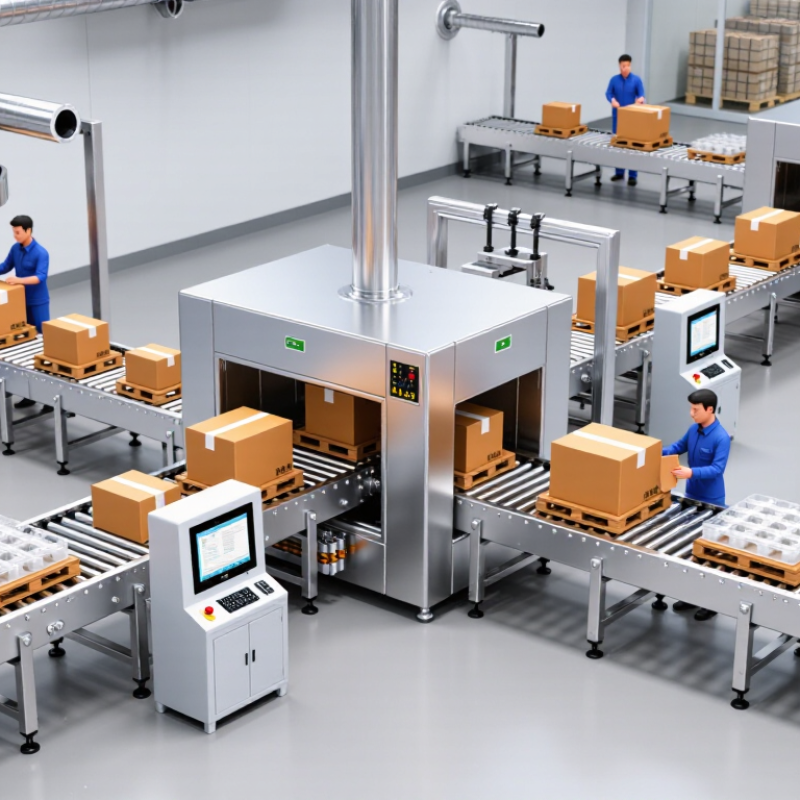
Define Your Product and Production Line Requirements
Start by documenting the product’s weight range, dimensions, shape, and packaging material. A sealed pouch can shift or flex differently from a rigid carton, affecting how steadily it travels across the scale. Measure both. Include the lightest and heaviest products, not just the average unit. Small details matter, especially when packages have uneven bases or soft edges.
Next, define the production line’s actual operating conditions. Record conveyor speed, spacing between products, and the available distance before and after the weighing section. A checkweigher must capture each item without slowing the line or confusing adjacent readings. Note how products arrive, too: gentle, consistent spacing is different from a stream of closely grouped packs. If the line speed changes by shift, include that range in the specification.
Consider the surrounding environment and the equipment that must connect to the checkweigher. Dust, washdown, vibration, and temperature changes can influence the required construction and setup. Identify the reject method, such as a pusher or air blast, and confirm there is enough room for safe product removal. Provide sample packages for testing where possible. Paper specifications can miss real behavior; a slightly warped tray may travel unpredictably, and teams sometimes overlook this until installation. Record inspection data and the limits your process can reliably maintain.
How to Choose the Right Roller Checkweigher? - Define Your Product and Production Line Requirements
| Product / Pack Type |
Typical Pack Weight |
Example Pack Dimensions (L × W × H) |
Example Line Rate |
Roller / Conveyor Considerations |
Key Selection Requirement |
| Small corrugated cartons |
0.2–2 kg |
150–300 × 100–220 × 50–180 mm |
30–60 packs/min |
Use closely spaced rollers and stable side guides to prevent small cartons from skewing or rocking. |
Confirm the minimum pack size, spacing, and required weighing tolerance at operating speed. |
| Medium shipping cases |
2–15 kg |
250–500 × 180–350 × 100–350 mm |
20–45 cases/min |
Allow enough weigh-section length for the entire case to be supported during measurement. |
Check maximum load, case stability, and the available conveyor length before and after weighing. |
| Large or heavy cartons |
15–50 kg |
400–800 × 300–600 × 150–600 mm |
8–25 cases/min |
Specify a frame and rollers rated for the maximum product load; consider controlled accumulation and transfer gaps. |
Size the system for the heaviest case and verify that upstream and downstream conveyors can handle it. |
| Rigid plastic crates or totes |
5–30 kg |
300–600 × 200–400 × 100–350 mm |
10–35 totes/min |
Check whether the tote base is flat and rigid; uneven feet or a flexible base can affect repeatability. |
Test representative empty and loaded totes, including the actual orientation and spacing. |
| Bagged products in cases |
1–20 kg |
250–600 × 180–450 × 100–400 mm |
10–30 cases/min |
Ensure cases do not deform or shift as they pass over roller transfers and weighing sections. |
Evaluate pack movement, product settling, and vibration from nearby machinery during trials. |
| Palletized unit loads |
Typically hundreds of kilograms or more |
Depends on pallet and load configuration |
Application-specific; usually much slower than case checkweighing |
Requires a heavy-duty, pallet-rated weighing solution and suitable powered roller sections. |
Confirm load rating, pallet dimensions, load distribution, and whether a roller checkweigher is the appropriate configuration. |
| Products for washdown areas |
Depends on pack type |
Depends on pack type |
Set by the production line |
Specify materials, seals, drainage, and cleaning compatibility appropriate to the actual washdown routine. |
Define cleaning chemicals, water exposure, temperature, and required ingress-protection level with the supplier. |
Planning note: The weights, dimensions, and rates above are example ranges for requirement definition, not performance guarantees. Confirm actual product samples, line speed, product spacing, environmental conditions, and weighing tolerance through application testing. Measurement performance depends on the product, system configuration, installation, and operating conditions.
Determine the Required Weight Range, Accuracy, and Throughput
How to Choose the Right Roller Checkweigher?
Determine the Required Weight Range, Accuracy, and Throughput
Choosing a roller checkweigher starts with the product, not the machine’s maximum rating. Define the lightest and heaviest packages that will pass through it, including packaging changes and normal fill variation. A 250-gram pouch and a 12-kilogram carton may need different load cells or conveyor setups. Leave sensible headroom, but do not choose an oversized range automatically; small weight changes can become harder to resolve. Small details matter.
Accuracy should match the decision the line must make. If a process target is ±2 grams, ask whether the complete system can hold that tolerance at operating speed—not only during a slow test. Product spacing, vibration, belt condition, and settling time can all affect readings. Check the stated accuracy conditions and request a trial with representative products. A clean, dry sample may behave differently from a warm, flexible package. That difference is easy to miss.
Throughput means stable packages per minute, not just a headline speed. Include the time needed for weighing, rejection, and spacing between products. A line running 90 cartons per minute may need more capacity if cartons arrive in clusters. Match belt length and reject timing to the actual layout, then allow for brief surges. Recheck these assumptions after a shift; real product flow is rarely perfectly even. The numbers deserve a second look.
How to Choose the Right Roller Checkweigher?
Compare the product weight range, indicative accuracy goal, and line throughput before selecting a system.
These are illustrative planning examples, not guaranteed equipment specifications. Actual throughput and weighing accuracy depend on product shape, spacing, conveyor conditions, and the applicable verification requirements. Confirm performance with representative products and operating conditions.
Choose a Roller Checkweigher Configuration and Conveyor Design
Choose the roller checkweigher around the products and line conditions, not just the target speed. Measure the shortest and longest packs, their base width, weight range, and surface stability. A narrow carton may wobble across widely spaced rollers, while a flexible pouch can sag between them. As a starting point, many roller-conveyor designs support a rigid item on at least three rollers; validate that spacing with actual products. Test the extremes. The weighing section also needs clear infeed and discharge transitions, so neighboring conveyors do not touch a pack during measurement. Accumulation pressure can disturb weight readings, so plan controlled spacing rather than letting cartons queue against one another.
MHI’s 2024 Annual Industry Report found that
55% of surveyed supply-chain leaders planned to invest more than $1 million in supply-chain technology over the following two years.
That broader investment trend makes integration worth planning early: specify conveyor height, speed control, side guides, and reject handling alongside the scale. Leave room for cleaning and maintenance access, especially around roller ends and the weighing platform. Small details matter. A design that handles today’s carton may struggle with a lighter, shorter pack next season. Run trials at minimum and maximum speeds, then review repeatability after changing product formats; one test on a perfect sample is not enough.
Assess Integration, Compliance, and Operating Conditions
A roller checkweigher should fit the line, not force the line into a redesign. Measure conveyor height, usable width, and the space needed for a reject device before comparing models. Check that the machine can communicate with the line controller and exchange clear run, fault, and reject signals. Measure twice. A small height mismatch can make packages tip or bounce, affecting readings and creating jams.
Compliance depends on the product and market, so confirm the required weighing accuracy, calibration process, and recordkeeping with your quality team. Ask how test weights are handled and whether results can be traced by time, product, and shift. For food or other washdown environments, inspect contact surfaces, drainage, and access for cleaning. A smooth-looking exterior is not enough if residue collects beneath rollers.
Operating conditions deserve a real trial. Test representative packages at the expected line speed, including light, heavy, soft, and uneven loads. Note nearby motors or floor vibration, which can disturb stable readings. Small gaps matter. Temperature changes, moisture, and frequent cleaning may also affect performance or maintenance needs. One awkward truth: a compact layout may save floor space but leave too little room for inspection and service. Allow technicians safe access, and confirm the equipment performs consistently under everyday conditions—not just during a short demonstration.
Compare Models and Verify Performance Before Purchase
Choosing a roller checkweigher means matching its performance to your actual line, not just comparing maximum speed. Check usable belt width, roller pitch, product spacing, package range, and reject timing. A long, soft pouch may behave differently from a rigid carton. Test both. OIML R 51-1:2006 classifies automatic catchweighers and addresses repeatability, eccentric loading, and influence factors. Use its requirements to compare specifications, but confirm which accuracy class and operating conditions apply to your product.
Before purchase, run representative packs at your intended line speed. Record average weight, standard deviation, missed rejects, and false rejects across repeated runs. Include light and heavy packs, and test after warm-up and during normal line vibration. These results reveal practical limits that a catalogue figure may not show. OIML R 51-1:2006 bases permissible errors on factors including load and verification scale interval; a single accuracy claim is not enough for a fair comparison.
Tips: Ask for a witnessed acceptance test using your own products. Keep the test settings and results. If space allows, trial the reject device and confirm every rejected pack reaches the collection point. Small details matter. A rushed test can miss drift, and real lines are rarely perfect.